

FANGKUAI Boiler is excited to announce its participation in the 2026 Indonesia International Boiler Exhibition (EXPO BOILER 2026), which will take place from November 3 to 5, 2026, at JIEXPO Jakarta International Expo, Indonesia.
As a professional industrial boiler manufacturer, FANGKUAI Boiler warmly welcomes customers, engineering companies, distributors, and industry professionals to visit Booth A3-74 to explore industrial boiler technologies and discuss customized heating solutions.
EXPO BOILER is an international exhibition dedicated to boiler technology, industrial heating systems, and related equipment. The event provides an opportunity for manufacturers, suppliers, and industrial users to exchange technical knowledge and explore business cooperation.
| Exhibition Name | EXPO BOILER 2026 |
|---|---|
| Exhibitor | FANGKUAI Boiler |
| Exhibition Date | November 3–5, 2026 |
| Location | JIEXPO Jakarta International Expo, Indonesia |
| Booth Number | A3-74 |
Industrial steam and heating systems play an essential role in manufacturing operations. Selecting the appropriate boiler technology can help businesses improve energy utilization, maintain stable production, and manage operating costs.
During EXPO BOILER 2026, FANGKUAI Boiler will introduce its industrial boiler solutions and share technical expertise with visitors from different industries.
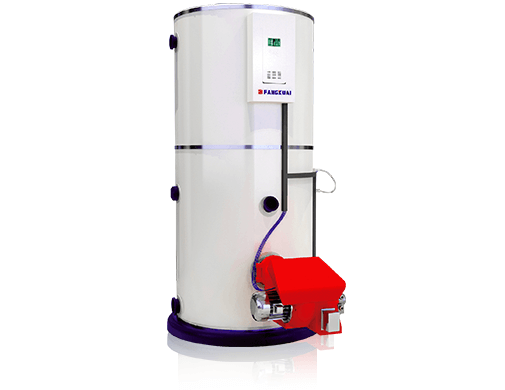
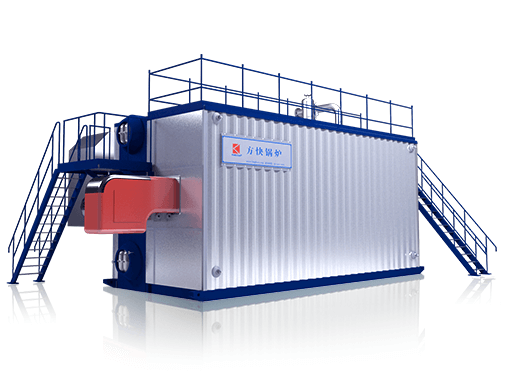
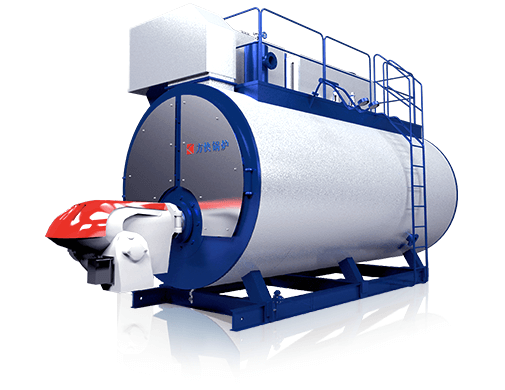
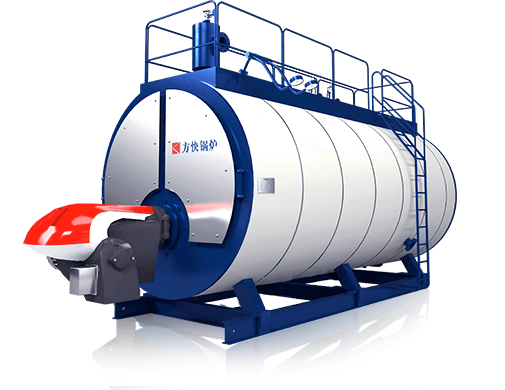
Our main product range includes:

Indonesia has a diverse industrial sector, including food processing, textiles, palm oil production, chemicals, and other manufacturing industries that require dependable steam and thermal energy.
FANGKUAI Boiler aims to support industrial customers by providing boiler equipment and technical solutions tailored to different production requirements.
At the exhibition, our technical representatives will be available to discuss important project considerations, including:
We welcome visitors to share their project specifications with our team so that we can discuss suitable equipment configurations and potential cooperation opportunities.
EXPO BOILER 2026 is an excellent opportunity to meet our team face-to-face, learn more about our industrial boiler products, and exchange ideas on industrial heating applications.
Whether you are looking for a new industrial steam boiler, considering an equipment upgrade, or searching for a long-term boiler manufacturing partner, we invite you to visit our booth in Jakarta.
Our team will be pleased to discuss your requirements and provide information about our products and technical services.
We sincerely invite our customers and partners from Indonesia and across Southeast Asia to meet us at EXPO BOILER 2026.
Exhibition: EXPO BOILER 2026
Date: November 3–5, 2026
Venue: JIEXPO Jakarta International Expo, Indonesia
Booth: A3-74
To arrange a meeting or discuss your industrial boiler requirements before the exhibition, please contact FANGKUAI Boiler through our official website.
We look forward to welcoming you at Booth A3-74 in Jakarta, Indonesia!


FANGKUAI Boiler is excited to announce our participation in the 140th China Import and Export Fair (Canton Fair 2026), which will be held from October 15th to 19th, 2026 at the China Import and Export Fair Complex in Guangzhou, Guangdong, China.
As a professional industrial boiler manufacturer, FANGKUAI Boiler will present our latest boiler technologies and customized heating solutions at Booth No. 6.1B03. We sincerely invite global customers, distributors, and industry partners to visit our booth and explore potential cooperation opportunities.
At Canton Fair 2026, FANGKUAI Boiler will showcase a variety of efficient and reliable boiler solutions designed for different industrial applications. Our products are developed to provide stable steam supply, energy efficiency, and flexible fuel options for customers worldwide.
Visitors can learn more about our main boiler products, including:
FANGKUAI Boiler provides heating solutions for various industries, including food processing, textile, pharmaceutical, chemical, manufacturing, and commercial heating applications. Our professional team can help customers select suitable boiler systems based on fuel type, steam demand, operating pressure, and project requirements.
The Canton Fair is an important international platform connecting manufacturers, buyers, and industry professionals from around the world. During the exhibition, visitors can communicate directly with the FANGKUAI Boiler team and discuss their specific heating and steam requirements.
Our experts will provide professional consultation on:
Whether you are planning a new boiler installation, replacing an existing heating system, or searching for a reliable boiler supplier, FANGKUAI Boiler is ready to provide professional support and suitable solutions.
With extensive experience in boiler manufacturing and international markets, FANGKUAI Boiler focuses on delivering safe, efficient, and environmentally friendly boiler equipment for customers around the world.
Through continuous innovation and cooperation with global partners, FANGKUAI Boiler aims to provide advanced heating technologies and professional services for different industrial sectors.
The 140th Canton Fair 2026 will be a great opportunity to explore new technologies, exchange industry insights, and develop future business partnerships.
We warmly welcome you to visit FANGKUAI Boiler:
Our team looks forward to meeting you at Canton Fair 2026 and discussing how FANGKUAI Boiler can support your industrial steam and heating needs.
See you at Canton Fair 2026!


September 24–27, 2026 | Booth 4A27 | Cairo International Conference Center (CICC), Egypt
Dabonn Energy is excited to announce its participation in EGYPT STITCH & TEX EXPO 2026, one of the leading textile machinery and technology exhibitions in North Africa and the Middle East. The exhibition will take place from September 24 to 27, 2026, at the Cairo International Conference Center (CICC) in Nasr City, Cairo, Egypt.
Visitors are warmly invited to Booth 4A27, where Dabonn Energy will present its latest industrial boiler technologies and energy-efficient steam solutions designed specifically for the textile industry.
Steam plays a critical role throughout textile manufacturing, including dyeing, printing, bleaching, washing, drying, and finishing. A reliable boiler system directly affects production efficiency, energy consumption, and operating costs.
At EGYPT STITCH & TEX EXPO 2026, Dabonn Energy will showcase a range of industrial boiler solutions engineered to meet the demanding requirements of textile factories, including:
Our engineering team will provide professional consultation to help visitors select the most suitable boiler system based on production capacity, fuel availability, steam demand, and energy-saving goals.
As textile manufacturers continue to pursue higher efficiency and lower operating costs, energy-saving boiler systems have become increasingly important.
Dabonn Energy integrates advanced combustion technology, intelligent control systems, and optimized heat transfer designs into every boiler solution. These technologies help customers achieve:
Whether powered by natural gas or biomass fuels, our industrial boilers are designed to deliver dependable performance while supporting sustainable manufacturing.
During the exhibition, visitors will have the opportunity to meet directly with Dabonn Energy's technical and sales specialists to discuss a wide range of industrial heating solutions.
Topics include:
Our team will also share successful application cases from textile manufacturers across different countries and explain how efficient boiler systems can improve productivity while reducing energy costs.
Egypt continues to strengthen its position as an important textile manufacturing hub in Africa and the Middle East. With increasing investment in textile production, the demand for reliable and energy-efficient steam generation equipment is also growing.
By participating in EGYPT STITCH & TEX EXPO 2026, Dabonn Energy looks forward to establishing new partnerships with textile manufacturers, engineering companies, distributors, and industrial investors throughout Egypt, North Africa, and neighboring regions.
We remain committed to delivering high-quality industrial boiler equipment backed by professional engineering support and comprehensive after-sales service.
We sincerely invite all visitors attending EGYPT STITCH & TEX EXPO 2026 to stop by Booth 4A27 and explore how Dabonn Energy can help improve the efficiency and sustainability of your textile production.
Exhibition: EGYPT STITCH & TEX EXPO 2026
Venue: Cairo International Conference Center (CICC), Nasr City, Cairo, Egypt
Date: September 24–27, 2026
Booth Number: 4A27
We look forward to meeting customers and partners from around the world and discussing innovative industrial boiler solutions for the future of the textile industry.